Configuration
Technical Insights
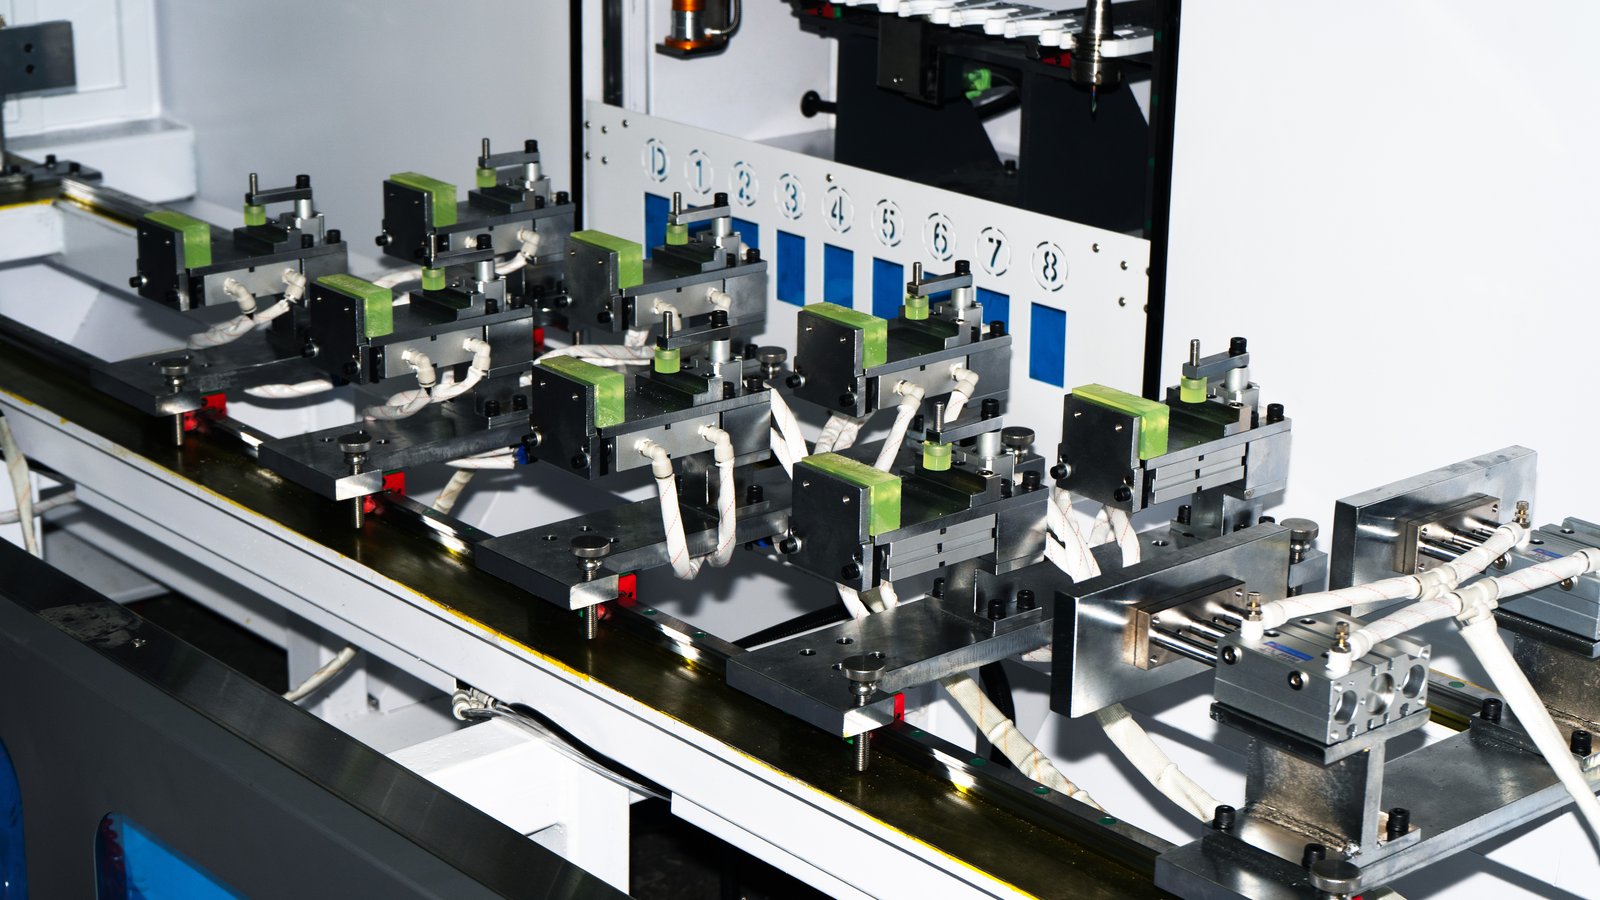
Automation frames, machine guarding, workbenches, display stands, all-aluminium furniture — orders like these share one profile: the sections vary wildly, batch counts are small, lead times are tight, and the next order may look nothing like the last one. Many shops buy on top spindle speed and headline accuracy, then six months later discover that what actually eats the margin is changeover, not cutting. A machine that changes over a dozen times a day can lose to one that changes over in five minutes, no matter how fast it cuts.
1. Changeover time comes down to three things
Break a changeover into three segments: programming and program retrieval, clamping and alignment, and tool preparation. Whichever segment is longest is your bottleneck.
- Programming: can it be generated from a graphical interface or a template library instead of hand-written every time?
- Fixturing: can modular fixtures with locating pins remove the need to indicate the part in?
- Tooling: are there enough pockets, and do the common tools stay resident to avoid re-setting?
2. The programming barrier: the most underestimated buying criterion
High-mix low-volume shops often have no dedicated programmer. A spec sheet saying "supports G-code" does not mean anyone on the floor can write it. This single factor decides whether the machine actually runs.
- Prioritise graphical programming, parameterised templates and profile section libraries that lower the skill floor
- Check whether the system supports barcode-triggered program recall — scan the profile, load the matching program
- Estimate training time: how long from zero to programming unaided?
- Ask whether the builder supplies program authoring and process support, not just the machine
3. Magazine capacity: adequate beats large
High-mix work invites two mistakes: a magazine too small, so every changeover means reloading tools; or an oversized magazine paid for pockets you never use, with a longer change path as a bonus.
- First count how many tools your common operations actually need — eight to twelve covers most cases
- An inline magazine has a short change path and suits lines with a stable tool set
- Watch time per tool change; at volume the accumulated effect is substantial
- Standardise tooling to reduce dependence on specials
4. Small batches need mistake-proofing too
Some argue that small batches do not justify error-proofing. The opposite is true: high changeover frequency raises the error rate, and one error usually scraps the whole batch.
- Inspect and record the first piece, always
- Control program versions: every edit gets a revision, and the floor only uses the latest
- Sample critical dimensions and log the drift trend
- Build foolproofing into the fixture so a reversed part will not seat
5. When to move from a general-purpose machine to a dedicated line
The strength of a general-purpose three-axis machine is its range; the price is changeover time. When a particular section's volume climbs steadily and keeps the machine occupied, it is time to pin it down and hand that work to more dedicated equipment. The test is simple: add up the annual machining hours for that part family. If it already takes a large share of the machine's effective annual hours, dedicated investment usually pays back.
Operation consolidation: what one machining centre replaces
| Original operation | Previous equipment | Covered in one set-up? | Main benefit |
|---|---|---|---|
| Sawing to length | Band saw / circular saw | Partly (cut first, or choose a long-travel model) | Fewer set-ups and less handling |
| Drilling | Pillar drill / radial drill | Yes | Hole pitch controlled by program — no marking out or templates |
| Slot and face milling | General milling machine | Yes | Consistent slot width and depth, fewer tool touches |
| Tapping | Tapping machine / by hand | Yes (rigid tapping) | Consistent threads, less rework on torn threads |
| Deburring / chamfering | Manual | Yes (chamfer tool) | One manual operation removed |
| Marking | Manual labels | Optional (marking or scribing tool) | Traceability marked in-process, no manual labelling |
FAQ
- How many axes do I need for high-mix low-volume work?
- If the work is mainly regular sections (square tube, I-beam, channel), three axes with a flip or indexing fixture covers most operations. Move to four or five axes only when you need free-form surfaces or multi-angle features on side walls. Do not chase axis count — programming complexity and machine cost both go up.
- What counts as a reasonable changeover time?
- It depends on the fixturing. With modular fixtures, locating pins and barcode program recall, a few minutes for a simple section change is achievable. If every changeover means re-indicating the part, ten or twenty minutes is common. Before buying, ask the builder to run a real changeover using one of your own parts.
- What if we have no programmer?
- Choose a control with graphical programming and process templates, and require training plus initial program authoring from the builder. Build a template library for your common sections; after a few rounds you stop depending on outside help.