Maintenance
Technical Insights
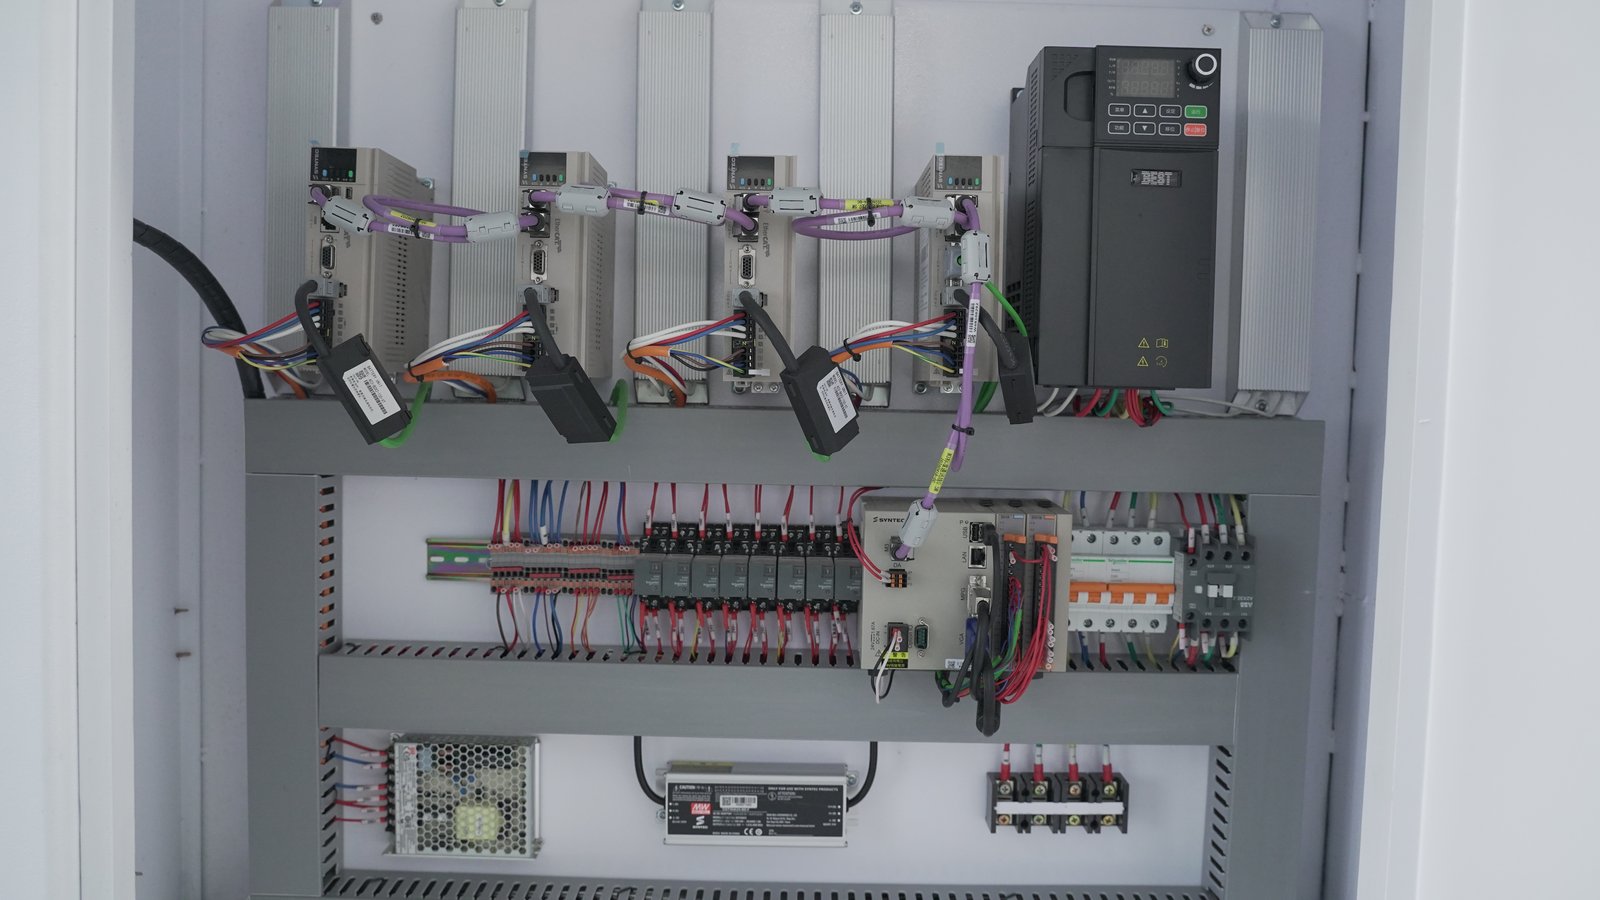
Most unplanned downtime on machining centres is not caused by a part failing suddenly, but by small daily tasks skipped for months: a taper never wiped, chips never cleared, lube level below minimum. Each omission looks harmless on its own; accumulated, they surface as lost accuracy or alarms.
Before every shift (about 10 minutes)
- Wipe the spindle taper and toolholder taper; confirm no chips or scoring
- Confirm air pressure meets specification and drain the filter regulator
- Check lubrication level and top up if below the minimum mark
- Clear chips from the table and fixtures, especially locating faces
- Run a dry home cycle and listen for abnormal noise on any axis
Weekly
- Clean the coolant tank strainer; check coolant concentration and condition
- Clean cabinet intake filters — dust inside raises failure rates
- Check the chip conveyor runs freely with no binding
- Spot-check repeat positioning accuracy and log the result
Monthly
- Check guideway and ballscrew lubrication; wipe old grease and reapply
- Tighten electrical terminals and earth bolts — vibration loosens them
- Back up machine parameters and part programs
- Log alarms and downtime for the month to guide next month's checks
Three maintenance cycles: tasks, time and owner
| Cycle | Main tasks | Time | Owner |
|---|---|---|---|
| Every shift | Taper wipe, air pressure, guideway oil level, chip removal | About 10 min | Operator |
| Weekly | Filter cleaning, fixture accuracy check, coolant concentration | About 30 min | Operator / team lead |
| Monthly | Guideway grease, screw and rack inspection, cabinet dust removal | About 2 h | Maintenance technician |
The most overlooked item: spindle taper cleaning
A single chip trapped between taper and toolholder makes the tool run out, showing up as oversized holes, chatter marks and rapid tool wear. This is hard to trace through parameters, yet prevented by one wipe before starting. Machines with frequent tool changes need it most.
Print these three lists and post them next to the machine. It works better than any maintenance policy: whether a task was done is obvious at a glance.
Frequently asked questions
- How often should the spindle taper be cleaned?
- Once before every shift, and every four hours on machines with heavy tool change duty. Wipe the taper with a lint-free cloth and a little cleaner, and check for fretting marks or rust. A single aluminium chip trapped in the taper is enough to make the tool run out.
- Does maintenance downtime hurt output?
- Ten minutes per shift is normally absorbed into the warm-up period before cutting starts. Skipping it costs far more through unplanned stops and accuracy drift than the ten minutes ever would.
- When should grease and coolant be replaced?
- Grease on the manufacturer interval, or earlier if the axis feels stiff or noisy. Coolant by concentration and smell: below the lower limit, or with odour or excess foam, replace the whole tank rather than topping up with concentrate.
- Can the operator do all of this?
- The first two cycles yes; the monthly items (screws, rack, cabinet) should go to a maintenance technician. Post the list at the machine with a signature column — it is far more effective than a policy document.